

 English
 中文简体
 русский
 Español
 Français
 عربى
 Português
 हिंदी
 Indonesia
 فارسی
 Tiếng Việt
 Türk


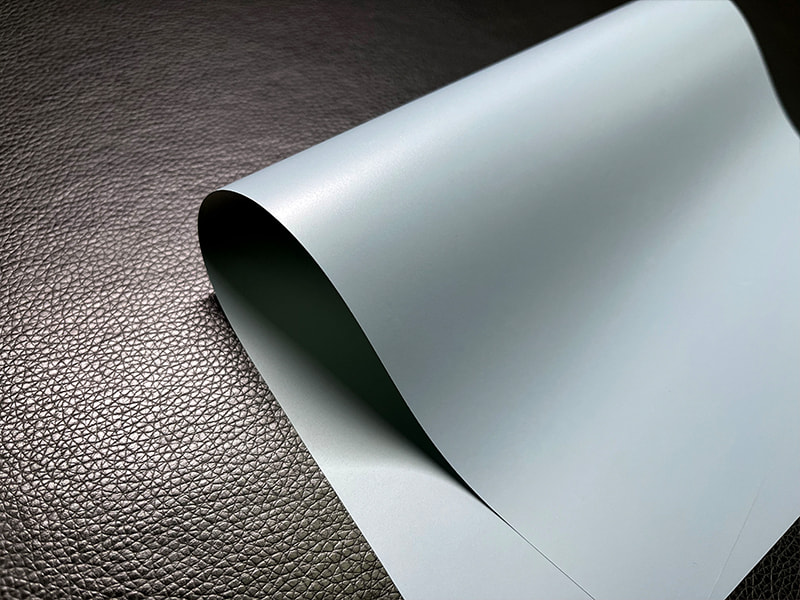
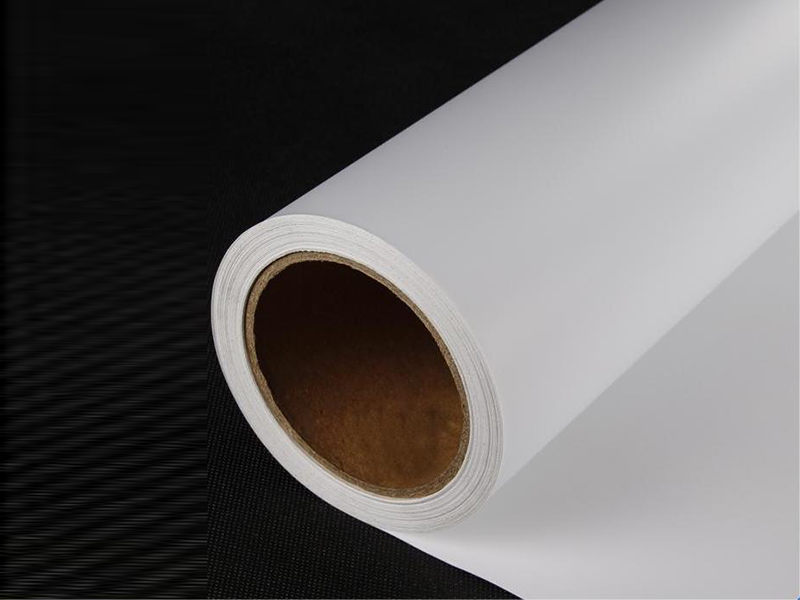
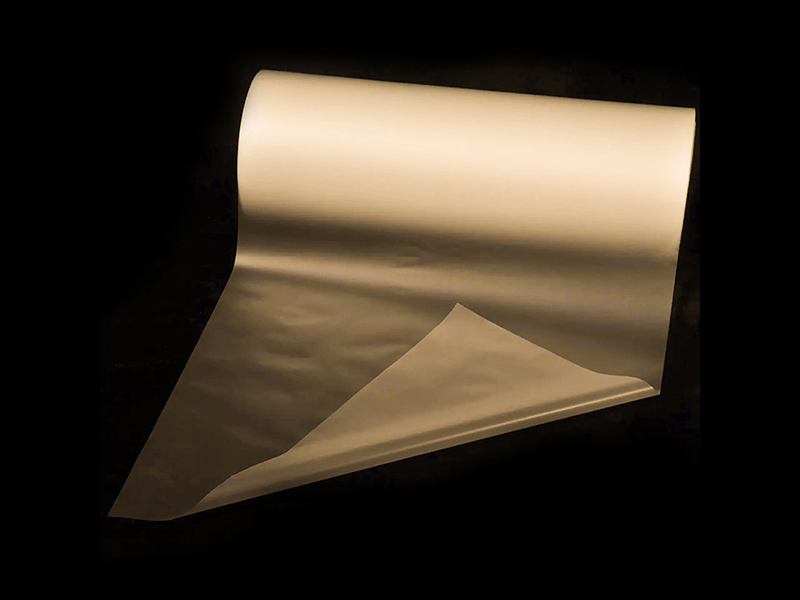
Matte Anti-Scratch Film for SPC
Matte Anti-Scratch Film for SPC is a transparent polyvinyl chloride overlay film applied to the surface of stone plastic composite flooring to reduce surface gloss and improve resistance to scuffing, abrasion, and fine scratches. The film is produced at thicknesses of 0.07 mm to 0.20 mm with a matte-finished surface, and gloss levels are controlled to between 5 and 20 gloss units. A hard coat, typically UV-cured polyurethane or acrylic, is applied to raise surface hardness while preserving the low-sheen appearance. The film is supplied in rolls for continuous lamination onto SPC plank and tile lines, and is specified where a wood or stone visual requires a low-reflection finish and where the floor must hold its appearance under commercial traffic.
Custom Film Development for SPC Producers
Matte Anti-Scratch Film for SPC is produced under an ODM/OEM arrangement. Gloss level, hard coat chemistry, film thickness, roll width, and color tint are configured to the flooring producer's substrate and lamination line. Buyers who are developing a new visual can request a matched film sample that reproduces the intended matte sheen on their plank or tile surface, and the approved sample becomes the production standard.
What Matte and Anti-Scratch Mean Together
Matte Surface Function
The matte finish scatters reflected light rather than producing a mirror image. On SPC flooring, this reduces glare from windows and overhead lighting and hides fine surface marks that show clearly on gloss surfaces. The matte texture is created by embossing the film or by adding a matting agent to the hard coat, and the chosen method determines how the finish behaves after cleaning and wear.
Anti-Scratch Function
Scratch resistance is provided by the hard coat layer, not by the matte texture alone. A UV-cured topcoat raises surface hardness to 2H to 3H pencil and controls the depth of marks left by grit, furniture feet, and cart wheels. The coat is applied at a dry film weight calibrated to the abrasion target, and adhesion to the PVC base film is verified by cross-hatch testing before the roll leaves the plant.
Specification Table
| Base Film | Polyvinyl chloride overlay film |
| Film Thickness | 0.07 mm to 0.20 mm |
| Gloss Level | 5 to 20 gloss units at 60 degrees |
| Hard Coat Type | UV-cured polyurethane or acrylic |
| Pencil Hardness | 2H to 3H |
| Taber Abrasion (H-18, 500 g) | 500 to 2,000 cycles |
| Cross-Hatch Adhesion | 5B to ASTM D3359 |
| Roll Width | 1.0 m to 2.0 m |
| Roll Length | Up to 300 m |
| Lamination Method | Hot-melt, heat-activated, or UV-cured bonding |
| Fire Classification | EN 13501-1 Bfl-s1 (assembly dependent) |
Lamination Context on SPC Lines
Substrate Preparation
SPC core boards are checked for surface flatness, moisture content, and residual dust before the wear layer is applied. Matte films show substrate imperfections through the film more than gloss films do, so surface condition at this stage determines the final visual quality.
Adhesive or Heat Bonding
Matte Anti-Scratch Film for SPC is bonded by hot-melt adhesive, heat-activated adhesive, or direct heat lamination depending on the line configuration. Bond strength is verified by peel testing on line samples, and the matte surface must remain free of adhesive strike-through after bonding.
Post-Lamination Inspection
Laminated planks are inspected for gloss uniformity, scratch marks introduced during handling, and edge lift. Gloss measurements are taken across the plank width and along the length to confirm the matte grade remains within the approved range after bonding.
Procurement Questions
How is the gloss level matched to an existing SPC product?
The buyer provides a finished plank sample or a gloss target in gloss units. The factory produces film samples at the target and measures them at 60 degrees against the buyer's sample. Once the gloss is approved, the matting agent or emboss depth is locked and recorded on the production sheet. Gloss is rechecked on each production lot using the same measurement geometry.
Does the matte finish wear away in traffic areas?
The matte appearance is generated by the surface texture or the coating formulation, and both are designed to remain stable under cleaning and foot traffic. Abrasion testing of the laminated product, not just the film, is the appropriate verification. Buyers should require the film supplier to supply Taber abrasion and gloss retention data for the completed assembly after 1,000 cycles.
What causes visible scratches to appear after installation?
Scratches that appear after installation usually originate from grit trapped under furniture feet, from installer tools contacting the floor, or from insufficient hard coat thickness for the traffic level. Once the origin is identified, the remedy is either a higher-abrasion hard coat grade or a maintenance protocol that includes grit removal at entrances. Scratch marks that show on the film surface are shallower than marks on uncoated PVC.
Can the film be supplied with a tint or color?
Yes. The base film can be tinted to adjust the color of the underlying SPC print, and the tint is specified in the same way as the gloss level. Buyers should provide a finished sample as the reference, because the tint is viewed through the film and its apparent color shifts with the hard coat thickness and substrate print underneath.
Handling and Storage
- Store Matte Anti-Scratch Film for SPC rolls in a clean, dry room at 15°C to 25°C and 40% to 60% relative humidity. Keep rolls upright and never lay them on their side, because edge compression leaves marks that remain visible after lamination.
- Allow rolls to reach line temperature for 12 hours before lamination. Cold film is stiffer and produces higher unwinding tension, which can stretch the film and alter the matte gloss appearance.
- Handle rolls with core supports and avoid dragging the film surface across pallet edges. The hard coat resists scratches from normal handling, but direct impact marks are permanent and cannot be buffed out.
- After lamination, clean the floor with a neutral detergent solution and a soft mop. Do not use abrasive pads or solvent-based cleaners, which dull the matte finish unevenly and reduce the anti-scratch performance of the hard coat.
- Keep partially used rolls wrapped and labelled. Dust that settles on the film surface is pressed into the matte texture during lamination and cannot be removed without affecting the gloss uniformity of the finished plank.